Address
Nanlang Industrial Zone, Xingtan Town, Shunde District, Foshan, Guangdong, China
Work Hours
Mon–Fri, 9:00 AM – 6:00 PM (CST/UTC+8). We aim to respond to all inquiries within 48 hours.

Address
Nanlang Industrial Zone, Xingtan Town, Shunde District, Foshan, Guangdong, China
Work Hours
Mon–Fri, 9:00 AM – 6:00 PM (CST/UTC+8). We aim to respond to all inquiries within 48 hours.
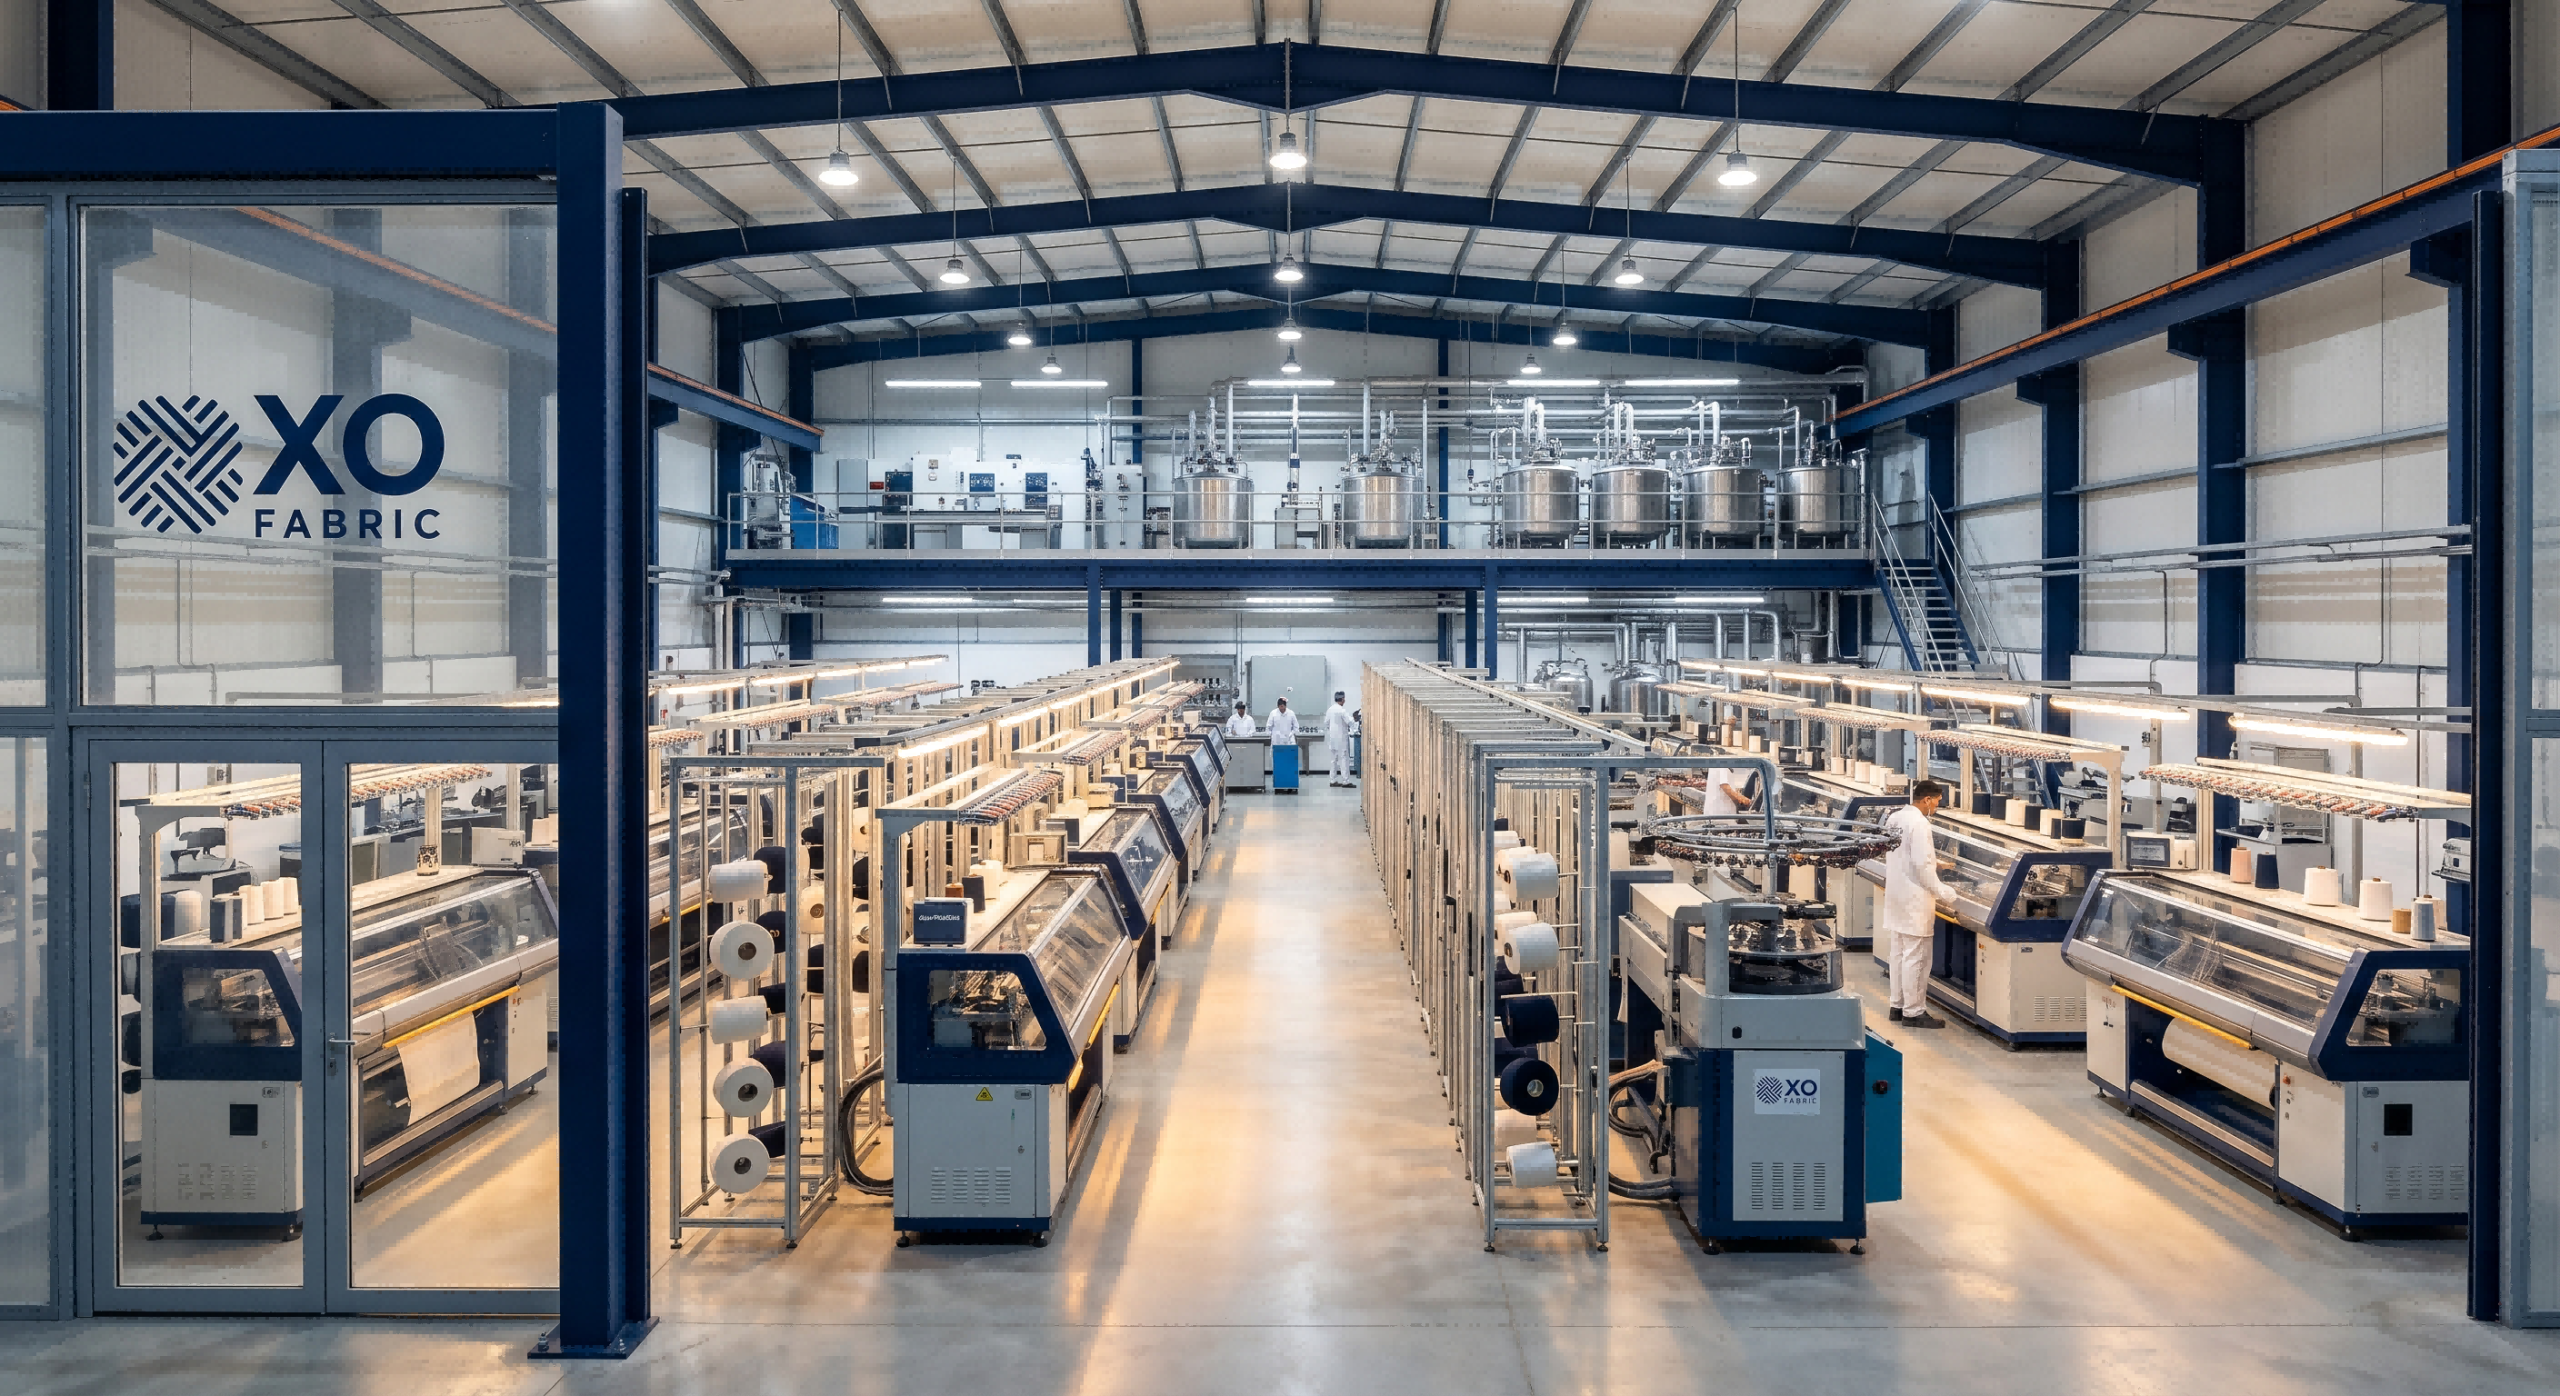
Supply chain transparency isn’t just a buzzword anymore—it’s a practical necessity for designers who need to trust where their materials come from. That’s why we’re pulling back the curtain on our textile manufacturing facility.
Since 2005, XO Fabric has operated on a simple philosophy: open manufacturing builds better partnerships. This tour walks you through knitting, dyeing, flocking, quality control, and logistics—the real workflow behind every meter of fabric we ship.
Whether you’re a procurement manager vetting suppliers or a designer specifying materials for a new collection, seeing the process firsthand helps you make smarter decisions. Let’s dive in.
Walk into the knitting floor and you’ll notice two things immediately: the rhythmic hum of circular machines and the precise organization of yarn cones. We run both single-jersey and interlock circular knitters alongside warp knitting equipment for stability-critical applications.
The process starts before the first stitch. Raw yarn gets inspected for evenness, tensile strength, and moisture content. A batch with inconsistent twist can cause barre stripes later—something we catch early with simple tension tests.
During knitting, operators monitor three key metrics in real-time:
For designers, this matters when you’re choosing between a 180 GSM jersey for drape versus a 280 GSM interlock for structure. I’ve seen projects fail because the spec sheet said “knit” without clarifying construction. Our Knit Products range covers both, but the decision tree starts with your end-use.
Quick troubleshooting note: if you notice curling edges on cut panels, check the stitch length first. A 2.8mm stitch on a lightweight single jersey will behave very differently than the same stitch on a double-knit. Sometimes the fix is as simple as adjusting the take-down roller pressure.
We handle everything from 500-meter sample runs to full container orders. The same QC checkpoints apply either way, which is non-negotiable for the mill. Consistency isn’t a premium feature—it’s the baseline.
Color is where theory meets reality. Our piece dyeing workflow follows a strict sequence: scouring to remove oils, dyeing in temperature-controlled vats, thorough washing, drying, and finishing. But the magic happens in the color matching lab.
When a client sends a Pantone code or a physical swatch, lab technicians start with spectral analysis. They account for substrate differences—a polyester flock won’t absorb dye the same way as a nylon base. This is where experience trumps software.
We maintain a library of over 2,000 custom formulas, but replication isn’t just about matching the recipe. Factors like water hardness, dye bath pH, and even ambient humidity can shift the final shade. That’s why we run strike-offs under the same conditions as bulk production.
For custom color work, our Piece Dyeing Service for Custom Colors includes three rounds of lab dips before bulk approval. It sounds cautious, but I’d rather spend an extra week getting the shade right than ship something that looks “close enough” under showroom lighting.
Color fastness testing happens in parallel. We test for:
One project that sticks with me: a hospitality client needed a deep navy that wouldn’t fade under UV-exposed lobby lighting. The first lab dip looked perfect under D65 lighting but shifted purple under warm LED. We adjusted the dye combination, added a UV-absorbing finish, and re-tested.
The compromise? A slightly higher cost per meter, but zero complaints after two years in service. That’s the kind of decision-making that doesn’t show up on a spec sheet. It required balancing aesthetic goals, performance requirements, and budget constraints—a very real trade-off.
On the sustainability side, the facility has reduced water consumption by 40% since 2020 through closed-loop rinsing systems. Non-toxic, low-impact dyes are standard for most orders unless a specific performance requirement dictates otherwise.
Flocking looks simple from the outside—tiny fibers standing upright on fabric—but the engineering behind consistent adhesion is anything but. Our process breaks down into four controlled stages.
First, adhesive coating. The viscosity matters: too thin and the flock penetrates too deep, losing that plush surface feel; too thick and you get uneven coverage. We target 3,500-4,200 cP depending on fiber length.
Next, electrostatic application. The flock fibers get charged and align perpendicular to the fabric surface in a high-voltage field. This is where even distribution happens. If the voltage fluctuates, you’ll see patchy areas or “bald spots” after curing.
Curing locks everything in. Temperature and time are calibrated to the adhesive chemistry—typically 150-165°C for 90-120 seconds. Rush this step and adhesion suffers; over-cure and the base fabric can yellow.
Final inspection checks for three things: adhesion strength (we target >3.5N/25mm peel resistance), visual uniformity under angled light, and hand feel consistency across the roll.
Our Flocked Products span applications from automotive headliners to fashion accessories. The customization options are broad: flock length from 0.3mm to 3.0mm, custom color matching, patterned adhesion for textured effects, and adhesive formulations tuned for flexibility or rigidity.
Here’s a real-world hiccup: a client requested a metallic silver flock for evening wear. The first production run looked stunning in the warehouse but showed adhesive bleed-through after garment pressing. The issue? The adhesive wasn’t fully compatible with the metallic coating on the fibers.
We reformulated the adhesive blend, added a brief pre-cure cooling step, and re-ran the batch. The lesson: always test finishing processes (pressing, steaming, washing) on actual production fabric, not just lab samples. Sometimes the messy middle is where the real learning happens.
For designers specifying flocked fabrics, consider the end-use abrasion. Upholstery needs higher adhesion strength than decorative apparel. If you’re unsure, ask for a swatch and do a simple rub test with a white cloth—any transfer means the surface isn’t fully cured.
Quality isn’t a final checkpoint; it’s woven into every stage. But dedicated QC stations catch what in-process monitoring might miss.
At each phase—post-knitting, post-dyeing, post-flocking—samples undergo standardized testing. The supplier follows ISO and ASTM protocols because international buyers need documentation that travels with the fabric.
| Test Parameter | Standard Method | Acceptable Range |
| Shrinkage (warp) | ISO 5077 | -2% to +1% |
| Shrinkage (weft) | ISO 5077 | -3% to +2% |
| Flock Adhesion | Internal Peel Test | >3.5N/25mm |
| Color Fastness (Wash) | ISO 105-C06 | Grade 4-5 |
Core tests include tensile strength (warp/weft, minimum 250N for apparel weights), shrinkage rate (target: <3% after three wash cycles), color fastness, flock adhesion, and visual inspection under 500-lux lighting for defects.
One nuance: shrinkage testing isn’t one-size-fits-all. A fabric destined for structured blazers gets tested with dry cleaning simulation; activewear gets wash-and-tumble cycles. The “right” test depends on your care instructions.
If a batch fails any metric, it doesn’t ship. Period. The mill would rather delay an order than compromise on consistency. For deeper details on protocols, the post on quality control processes breaks down the testing equipment and frequency.
From a designer’s perspective, this rigor means you can specify with confidence. If the swatch you approved meets the spec, the bulk order will too. That predictability is worth more than a marginal cost saving.
Finished fabric doesn’t just get stacked and shipped. Climate-controlled warehouse facilities maintain 20-22°C and 45-55% relative humidity to prevent moisture-related issues like mildew or dimensional shifts.
Inventory management is fully digital. Every roll gets a barcode linked to its production batch, test results, and location. When an order comes in, the system allocates stock in real-time, reducing picking errors and speeding up fulfillment.
For global shipping, partnerships with multiple freight forwarders offer flexibility:
The facility handles orders of any size. A 50-meter sample run gets the same attention to packaging and documentation as a full container. That scalability matters when you’re prototyping a new collection and need to reorder quickly.
On-time delivery rate sits above 98% for B2B clients. The 2%? Usually external factors like port delays or customs holds—things the team can’t control but does proactively communicate about.
Pro tip for procurement teams: if you’re working with tight deadlines, build in a 3-5 day buffer for customs clearance, especially for first-time imports. All necessary documentation (commercial invoice, packing list, certificate of origin) can be provided in advance to smooth the process.
After walking through the facility, the value proposition is straightforward: transparency reduces risk, consistent quality reduces rework, and reliable logistics reduce stress.
Getting started follows a simple three-step flow:
For custom projects, starting with a small trial order before scaling is recommended. It’s a low-risk way to validate performance in your specific manufacturing environment.
If you’re ready to discuss your next textile project, reach out via the Contact page. Whether you need a quote, a custom development, or just want to schedule a virtual tour, the team is ready to help.
For more on why partnership matters in textile sourcing, the post on collaboration advantages dives deeper into models and long-term value.
Seeing how fabric is made changes how you specify it. That tension between ideal specs and real-world production constraints? It’s where good decisions happen. The facility isn’t perfect—no operation is—but the commitment to transparency means problems get solved collaboratively, not hidden.
Next time you’re evaluating a supplier, ask to see their process. Not just the finished product, but the in-between steps. The answers you get will tell you more about reliability than any brochure ever could. And honestly, that’s the kind of insight you can’t fake.