Address
Nanlang Industrial Zone, Xingtan Town, Shunde District, Foshan, Guangdong, China
Work Hours
Mon–Fri, 9:00 AM – 6:00 PM (CST/UTC+8). We aim to respond to all inquiries within 48 hours.

Address
Nanlang Industrial Zone, Xingtan Town, Shunde District, Foshan, Guangdong, China
Work Hours
Mon–Fri, 9:00 AM – 6:00 PM (CST/UTC+8). We aim to respond to all inquiries within 48 hours.
Double Knit Fabric: Apparel Uses, Benefits & Sourcing Guide. This guide covers key properties, real-world applications, and a practical sourcing checklist for B2B buyers.
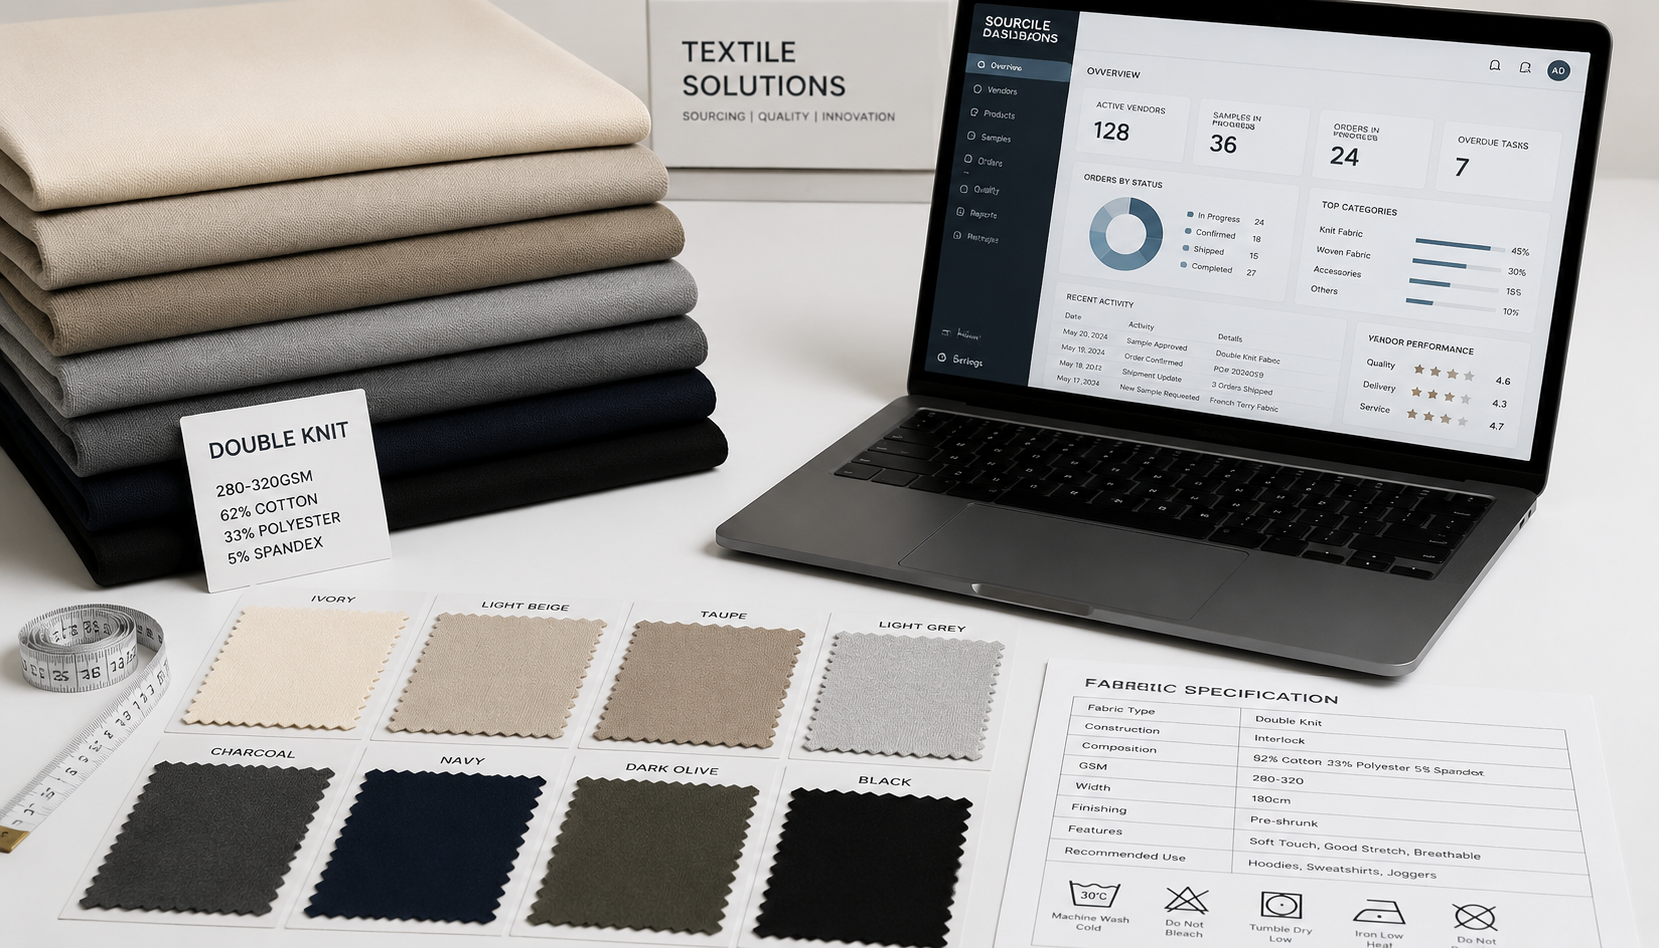
A European sportswear brand once ordered 12,000 m (39,370 ft) of what they called “double knit” fabric, only to receive an interlock structure that pilled aggressively after three washes. The term “double knit” gets thrown around interchangeably with interlock, Ponte, and rib-backed constructions, but they behave very differently on the cutting table and in the laundry. For B2B buyers, clarifying these distinctions before sampling can save months of revision cycles.
This guide breaks down what double knit fabric actually is, where it excels in apparel production, and how to source it without the common pitfalls that derail development timelines. We’ll cover structural definitions, performance parameters, application-specific recommendations, and a sourcing checklist you can hand to your procurement team today.
Here’s the uncomfortable truth: a significant percentage of spec sheets circulating through the global supply chain use “double knit” as a catch-all term for any fabric that looks thick and doesn’t curl. In practice, true double knit refers to a specific construction where two independent needle beds simultaneously form loops, and those loops are interconnected through tuck or miss stitches. This is fundamentally different from interlock, which uses a single needle bed with paired needles creating a double-layered rib structure.
The distinction matters enormously when you’re cutting 5,000 pieces. A true double knit’s interconnected loop architecture distributes stress across both faces, yielding superior abrasion resistance and dimensional stability. Interlock, while visually similar, relies on the mechanical interlocking of two 1×1 rib courses — it’s tighter than single jersey but structurally weaker under repeated lateral stress.
And then there’s Ponte di Roma, which is technically a double knit but uses a specific 2×2 rib face with a plain stitch back. It’s heavier, more rigid, and drapes differently than a jersey-face double knit. If your spec sheet just says “double knit,” you might receive any of these three constructions — and your garment fit will vary wildly.
| Comparison Dimension | True Double Knit | Interlock | Ponte di Roma |
|---|---|---|---|
| Needle bed configuration | Dual independent beds | Single bed, paired needles | Dual beds, 2×2 rib face |
| Loop interconnection | Tuck/miss stitches linking both faces | Mechanical interlock of two 1×1 ribs | 2×2 rib face + plain back |
| Face/back symmetry | Typically symmetrical | Symmetrical | Asymmetrical |
| Typical weight range (metric) | 200–400 gsm | 180–280 gsm | 280–380 gsm |
| Typical weight range (imperial) | 5.9–11.8 oz/yd² | 5.3–8.3 oz/yd² | 8.3–11.2 oz/yd² |
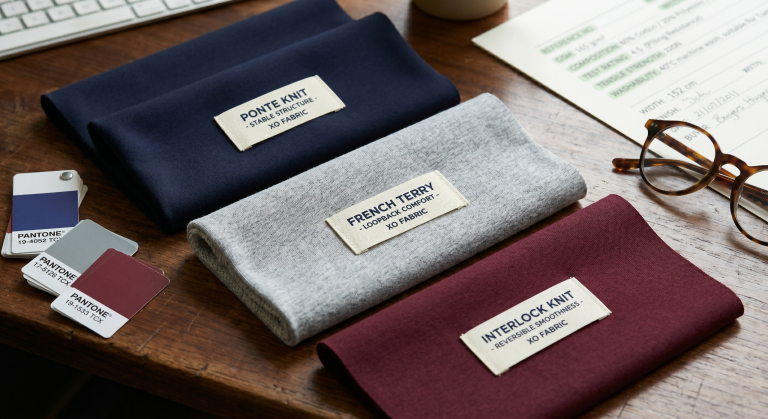
When a spec sheet says only “double knit,” you’re essentially handing the supplier a blank check on construction type. Two factories will deliver two entirely different fabrics, and your QC team will spend weeks reconciling the differences. Always specify the sub-type — jersey-face, rib-back, French terry, or Ponte — in your technical pack.
Gauge — the number of needles per inch (2.54 cm) on the knitting machine — is the single most influential variable in double knit construction. An 18-gauge (18G) machine produces a coarser, more open structure with a heavier hand feel, while a 28G machine creates a tighter, smoother surface that reads as more refined. The difference isn’t subtle; it’s the gap between a structured blazer fabric and a fluid dress weight.
On a dual-needle-bed machine, each face operates independently before the connecting stitches bind them. At 18G, you’re typically looking at finished weights of 300–400 Fabric GSM Calculator (8.9–11.8 oz/yd²) using conventional polyester or poly-cotton yarns. The loops are larger, the fabric breathes better, but the surface texture is visibly coarser. At 28G, the same yarn composition can yield 200–260 gsm (5.9–7.7 oz/yd²) with a much smoother face — ideal for tailored applications where drape and hand feel matter.
| Gauge | Typical Weight (gsm / oz/yd²) | Suited Yarn Types | Hand Feel Character |
|---|---|---|---|
| 18G | 300–400 / 8.9–11.8 | Spun polyester, poly-cotton blends | Structured, coarse, substantial |
| 22G | 250–320 / 7.4–9.4 | Ring-spun cotton, modal blends | Balanced, versatile, mid-weight |
| 28G | 200–260 / 5.9–7.7 | Filament polyester, Tencel blends | Smooth, refined, fluid drape |
The yarn you choose for double knit isn’t just a cost decision — it fundamentally reshapes the fabric’s behavior across its lifecycle. A 100% polyester double knit at 280 gsm (8.3 oz/yd²) delivers excellent dimensional stability and wrinkle recovery, but it traps body heat and can feel plasticky against the skin. Pure cotton double knits feel luxurious on first touch, but they shrink. According to AATCC TM 135, the industry standard for knitted textile dimensional changes, unmercerized cotton double knits routinely show 5–8% shrinkage after five wash cycles — unacceptable for most commercial apparel programs.
The sweet spot, in my experience, is a 70/30 poly-cotton blend with 3–5% elastane. You get the polyester’s stability (shrinkage under 3% per AATCC 135) combined with cotton’s moisture absorption and skin comfort. The trade-off is a slightly higher cost — typically 10–15% more than pure polyester — and a modest reduction in color vibrancy since cotton fibers absorb dye differently than polyester.
One critical point that gets overlooked: interlock knit fabric and true double knit are not interchangeable in yarn selection. Because interlock’s paired-needle structure creates less inter-yarn friction, it can use finer counts without sacrificing integrity. True double knit, with its more complex loop architecture, needs slightly higher twist yarns to prevent snagging during knitting. Specifying the same Yarn count for both constructions will yield very different results.
Double knit’s core value proposition for apparel manufacturers comes down to three measurable advantages. First, the no-curl edge. Single jersey curls aggressively at the selvedge — factories typically lose 3–5% of fabric width to curl-related cutting waste. Double knit lies flat, which means tighter marker layouts and better material utilization. On a 10,000-piece production run, that 3–5% translates directly into thousands of dollars saved.
Second, elastic recovery. A well-constructed double knit with 5% elastane content consistently recovers 92–96% of its original dimensions after 20% elongation. Single jersey with the same elastane content typically recovers 85–90%. That difference compounds over the garment’s lifecycle — double knit clothing maintains its shape through significantly more wear cycles.
Double knit isn’t universally superior — it carries real penalties that affect product positioning. The same dual-layer construction that provides stability and body adds weight. A 280 gsm (8.3 oz/yd²) double knit feels substantially heavier than a 180 gsm (5.3 oz/yd²) single jersey, which limits its viability for summer-weight T-shirts and lightweight base layers. Freight costs also increase proportionally — shipping 1,000 kg (2,205 lb) of double knit yields fewer linear meters than the same weight in single jersey.
Breathability is another concern. The interconnected double-face structure restricts airflow significantly. In controlled testing, double knit fabrics show 30–40% lower air permeability than equivalent-weight single jersey constructions. For activewear or hot-climate apparel, this can be a dealbreaker unless you specify an open-face construction like mesh or eyelet double knit.
There’s also a failure mode specific to high-gauge, lightweight double knits: layer separation. When the connecting stitches between the two faces are too few or too fine — common in cost-reduced 28G constructions — repeated aggressive washing can cause the faces to delaminate. This presents as bubbling or rippling on the fabric surface, and it’s essentially irreversible. Specifying a minimum connecting stitch density in your tech pack is the only reliable prevention.
For compliance-conscious buyers, it’s worth noting that OEKO-TEX Standard 100 certification applies equally to double knit and single-layer constructions. Always verify that your supplier holds current certification, particularly for products destined for the EU or children’s wear markets.
Which structure fits your product line? Rather than burying the answer in paragraphs, here’s the direct comparison:
| Selection Criteria | Double Knit | Single Jersey | Interlock |
|---|---|---|---|
| Weight range (metric/imperial) | 200–400 gsm / 5.9–11.8 oz/yd² | 120–220 gsm / 3.5–6.5 oz/yd² | 180–280 gsm / 5.3–8.3 oz/yd² |
| Cutting edge curl risk | Minimal — lies flat | High — aggressive curling | Low to moderate |
| Elastic recovery (%) | 92–96% at 20% stretch | 85–90% at 20% stretch | 88–93% at 20% stretch |
| Breathability rating | Low to moderate | High | Moderate |
| Typical price range | Higher (+15–25% vs single jersey) | Baseline | Moderate (+5–15% vs single jersey) |
| Best-fit applications | Blazers, joggers, structured dresses, uniforms | T-shirts, underwear, lightweight tops | Polo shirts, babywear, medical scrubs |
If your product needs structure without interfacing — think unstructured blazers, tailored joggers, or shift dresses — double knit is the clear winner. If you’re producing basic tees or underwear where drape and breathability dominate, single jersey remains unbeatable. Interlock occupies the middle ground: smoother than single jersey, lighter than double knit, but lacking the true structural integrity of a dual-bed construction.
Double knit’s resurgence in menswear isn’t accidental — it solves specific problems that woven fabrics and single knits can’t address. The structured-yet-comfortable blazer, the travel-friendly trouser, the polo that holds its collar shape after 50 washes — these are all products where double knit’s unique properties create measurable value.
For unstructured blazers, a jersey-face double knit at 280–300 gsm (8.3–8.9 oz/yd²) provides enough body to hold a shoulder line without shoulder pads, while the knit structure allows the kind of natural stretch that wovens simply cannot match. The key is balancing weight against drape — too heavy and the blazer reads as costume-like; too light and it collapses into a cardigan.
Joggers and performance trousers represent double knit’s sweet spot. A French terry double knit at 260–300 gsm (7.7–8.9 oz/yd²) offers the structured silhouette that separates premium joggers from gym sweats, while the looped interior provides moisture management. For golf and outdoor trousers, a poly-spandex double knit at 220–260 gsm (6.5–7.7 oz/yd²) delivers four-way stretch with enough recovery to maintain crease lines — a feature that pure elastane-blended single jerseys struggle to achieve.
| Application | Recommended Weight | Key Performance Requirement | Construction Type |
|---|---|---|---|
| Unstructured blazer | 280–300 gsm (8.3–8.9 oz/yd²) | Wrinkle resistance, drape, structure | Jersey-face double knit |
| Polo / collared knit | 200–240 gsm (5.9–7.1 oz/yd²) | Breathability, collar stability | Piqué-face double knit |
| Joggers / sweatpants | 260–300 gsm (7.7–8.9 oz/yd²) | Drape, elastic recovery | French terry double knit |
| Golf / outdoor trousers | 220–260 gsm (6.5–7.7 oz/yd²) | Four-way stretch, quick-dry | Poly-spandex double knit |
A mid-tier European brand ordering 8,000 m (26,247 ft) for their AW25 collection learned this the hard way. They needed a blazer-weight fabric that wouldn’t wrinkle in travel packaging. Their first attempt — 100% polyester double knit at 300 gsm (8.9 oz/yd²) — passed every drape test but trapped body heat so aggressively that wear-testers complained within 30 minutes. They pivoted to pure cotton double knit, which felt incredible on the body but wrinkled badly and shrank over 6% after five washes per AATCC 135 testing.
Their third attempt used a 2×2 rib-back double knit at 320 gsm (9.4 oz/yd²) — too stiff for the relaxed blazer silhouette they wanted. They finally settled on a jersey-face construction at 280 gsm (8.3 oz/yd²) in a 70/30 poly-cotton blend with a tighter 24G gauge and silicone softener finish. The result wasn’t perfect — the drape was slightly less fluid than their original 100% polyester goal, and material cost increased approximately 12%. But it passed AATCC 135 with under 3% shrinkage, achieved Martindale pilling resistance at 20,000+ cycles, and the hand feel satisfied their design team. Sometimes the right fabric is the one that compromises intelligently.
Women’s and children’s apparel presents different demands. Straight-cut dresses in double knit need higher elastic recovery to maintain silhouette through sitting and movement cycles. Children’s school trousers require extreme wash durability — 50+ industrial wash cycles without pilling or shape loss. In both cases, the specification conversation starts with wash performance, not hand feel.
The production advantage of sourcing from an integrated facility — one that handles everything from yarn preparation through knitting, dyeing, and finishing — becomes apparent in development speed. When the same team controls the yarn twist, gauge settings, and finishing parameters, iteration cycles compress from weeks to days. This matters enormously when you’re working toward seasonal deadlines.
The difference between a successful double knit procurement and a costly revision cycle almost always comes down to specification precision at the RFQ stage. Vague language in your tech pack is an invitation for suppliers to optimize for their margins, not your product requirements.
Before committing to large-volume orders, it’s worth requesting samples across 1–3 different weight and composition variations to validate performance under your specific testing protocols. Procurement teams can submit sampling requests through the factory’s contact portal, which supports a 3-step workflow: select specifications, submit the form, and confirm international logistics arrangements. Sample books are available for physical evaluation at no charge.
For procurement teams working with custom specifications or complex constructions, the factory’s technical engineering team provides feasibility assessments within 24 hours of receiving specification documents or design drawings through the same contact interface. This includes preliminary pricing guidance and lead time estimates based on current production capacity.
Double knit excels in applications requiring structure, wrinkle resistance, and dual-face usability. The most common double knit fabric apparel uses include unstructured blazers, tailored joggers, shift dresses, uniform trousers, and structured polo shirts. It’s not ideal for lightweight summer T-shirts, intimate apparel, or any product where maximum breathability and minimal weight are primary requirements.
Knit fabric spans nearly every apparel category, but the construction type must match the application. Single jersey dominates T-shirts, underwear, and lightweight layering pieces. Double knit takes over where structure and stability matter — outerwear, trousers, blazers, and performance sportswear. Interlock occupies the middle ground for polo shirts, babywear, and medical garments. The selection framework is simple: weight and structure requirements dictate construction choice.
No. Interlock is a single-needle-bed construction using paired needles to create a double-layered 1×1 rib structure. True double knit uses two independent needle beds that simultaneously form separate fabric faces, interconnected by tuck or miss stitches. Interlock’s seam strength and abrasion resistance are typically 15–20% lower than equivalent-weight true double knit. The terms are frequently confused in the industry, which is precisely why construction diagrams should be mandatory in every spec sheet.
Industry standard ranges break into three tiers: lightweight at 200–240 gsm (5.9–7.1 oz/yd²) for dresses and refined knit tops, midweight at 250–300 gsm (7.4–8.9 oz/yd²) for blazers, joggers, and structured trousers, and heavyweight at 300–400 gsm (8.9–11.8 oz/yd²) for outerwear, uniforms, and cold-weather applications. The right weight depends entirely on your end product — a blazer at 280 gsm (8.3 oz/yd²) and joggers at 280 gsm (8.3 oz/yd²) feel completely different because the yarn composition and finishing treatments vary.
Double knit isn’t a universal solution — it’s a specific tool for specific problems. When your product demands structure without rigidity, stretch without sagging, and a clean face on both sides, no other knit construction delivers the same combination. The key is specifying it precisely enough that your supplier can’t substitute a cheaper alternative, and testing it rigorously enough that your end customer never discovers a problem you could have caught at the sampling stage. Start with a clear spec sheet, validate with a pilot run, and let the test data — not the hand-feel swatch — make the final call.