Address
Nanlang Industrial Zone, Xingtan Town, Shunde District, Foshan, Guangdong, China
Work Hours
Mon–Fri, 9:00 AM – 6:00 PM (CST/UTC+8). We aim to respond to all inquiries within 48 hours.

Address
Nanlang Industrial Zone, Xingtan Town, Shunde District, Foshan, Guangdong, China
Work Hours
Mon–Fri, 9:00 AM – 6:00 PM (CST/UTC+8). We aim to respond to all inquiries within 48 hours.
Reflective Knit Fabric for Safety & Performance Apparel. This guide covers key properties, real-world applications, and a practical sourcing checklist for B2B buyers.
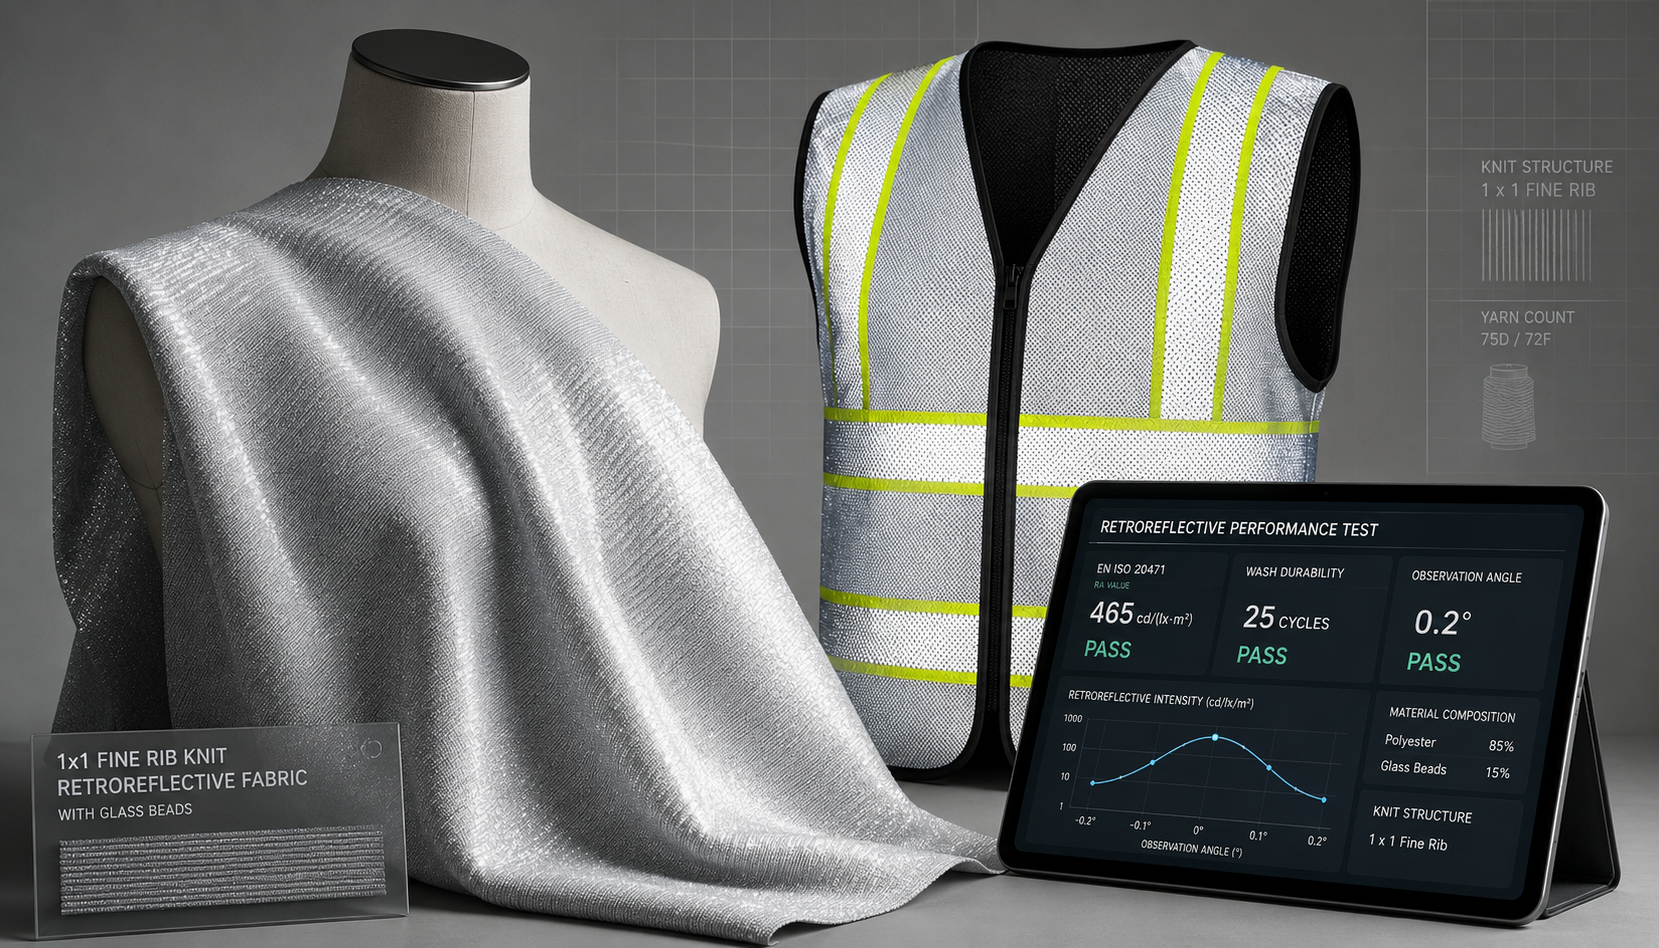
A German sportswear brand recalled 12,000 running vests in 2024 because their reflective panels lost 60% retro-reflectivity after just 15 wash cycles — falling below EN ISO 20471 Class 1 minimums. The root cause: wrong base knit paired with heat-transfer film. For B2B apparel buyers sourcing reflective knit fabric performance materials, understanding the interplay between substrate construction, reflective technology, and wash durability is the difference between a compliant product and a costly recall.
At its core, retro reflective fabric is a textile system — a base material combined with an optical layer. When we talk about reflective knit fabric, we are referring specifically to a knit substrate—usually a jersey, rib, or interlock construction—that has been bonded or coated with a layer containing micro glass beads or prismatic structures.
These microscopic elements act like tiny mirrors or lenses. When light hits them, it is captured and redirected back toward the source, regardless of the angle of arrival. This is why a runner’s vest glows when headlights hit it. However, the “knit” part of the equation is just as critical as the “reflective” part.
Woven reflective fabrics are stiff, stable, and durable, but they lack the mechanical stretch required for modern performance apparel. Knit substrates, conversely, offer inherent elasticity and drape. But this stretch creates a massive technical challenge: the reflective film must deform and recover without cracking or delaminating.
| Parameter | Reflective Knit | Reflective Woven |
|---|---|---|
| Stretch & Recovery | High (30–50% elongation) | Low (< 5%) |
| Breathability | High (Open loop structure) | Low to Medium |
| Weight | Light to Midweight | Heavy |
| Drape Conformity | Excellent (Body-hugging) | Stiff / Boardy |
| Typical Application | Sportswear, Active Safety | Heavy Workwear, Vests |
In the industry, you will hear terms like “silver reflective fabric” or “high visibility reflective fabric.” These are often used interchangeably in marketing, but technically, “silver” describes the color of the standard glass bead film, while “high visibility” refers to the combination of fluorescent background material and retro-reflective elements required by standards like EN ISO 20471.
When sourcing, it is vital to distinguish between a fabric that is merely shiny and one that provides true retro-reflection. If you are exploring options for base substrates, you can browse the performance knits catalog for base fabric candidates to see the range of constructions available.
There are two main technologies used to turn a stretchy knit into a safety signal: glass bead technology and micro-prismatic technology. Understanding the physics helps in selecting the right material for your specific end-use.
Glass Bead Film: This is the traditional “silver reflective” look. It uses microscopic glass spheres suspended in a binder. When light enters the bead, it refracts and bounces back. It is cost-effective and flexible, but the retro-reflection efficiency drops off sharply at wide entrance angles.
Prismatic Film: This uses cube-corner structures (tiny pyramids) to reflect light. It is significantly brighter than glass bead technology and maintains visibility at wider angles. However, prismatic films are thicker and stiffer, making them harder to apply to stretchy knits without compromising the fabric’s hand feel.
The application process is a high-stakes bonding operation. It generally follows these four steps:
| Parameter | Glass Bead Film | Prismatic Film |
|---|---|---|
| Retro-reflection (cd/lux/m²) | 100–330 | 330–1000+ |
| Wash Durability | 25–50 cycles | 50–100+ cycles |
| Flexibility on Knit | Good | Challenging (Stiffer) |
| Cost Tier | Low to Medium | High |
| Common Certification | EN 20471 Class 1/2 | EN 20471 Class 3 |
The construction of the base knit plays a massive role here. A loose single jersey might snag or distort under the heat press. A stable 1×1 rib, however, provides a smooth surface with vertical lines that help the adhesive key into the structure. The 1×1 fine rib knit is often cited as a compatible substrate because its balanced structure minimizes the “orange peel” effect where the film wrinkles due to uneven fabric tension.
When you specify reflective knit fabric performance, you cannot just look at a swatch under a flashlight. You need data. There are three non-negotiable metrics that define whether a fabric will pass a lab test or fail in the field.
1. Coefficient of Retro-Reflection (RA): Measured in candelas per lux per square meter (cd/lux/m²). This tells you how bright the fabric is. For EN ISO 20471 Class 1, the minimum is often around 100 cd/lux/m² after washing.
2. Wash Durability: How many cycles does it take for the RA to drop below the minimum? Industrial standards often require testing after 5, 25, or 50 washes at 60°C (140°F) or 75°C (167°F).
3. Stretch Compatibility: Does the film crack when the fabric stretches? A high-performance knit might stretch 50%, but if the film cracks at 20%, the garment is defective at the seams.
| Parameter | Industry Minimum | Premium Target | Test Standard |
|---|---|---|---|
| Retro-reflection (cd/lux/m²) | 100 | 330+ | EN 20471 / ANSI 107 |
| Wash Cycles (Industrial) | 25 | 50–100 | ISO 6330 |
| Tensile Retention | > 80% | > 90% | ASTM D5034 |
| Colorfastness | Grade 3–4 | Grade 4–5 | ISO 105-C06 |
| Stretch Recovery (%) | > 85% | > 95% | ASTM D2594 |
A common trap buyers fall into is assuming thicker film equals better performance. While a thicker prismatic film (0.5 mm / 0.02 in) offers higher brightness, it reduces the fabric’s breathability and can drop stretch recovery by 30% compared to a thinner glass bead film (0.2 mm / 0.008 in).
If you are calculating the final weight of your laminate, remember to account for the film weight. A base fabric of 180 gsm (5.3 oz/yd²) might become 240 gsm (7.1 oz/yd²) after lamination. You can use the GSM calculator to convert these weights and ensure your final garment doesn’t exceed weight targets.
How long does reflective clothing last? If the materials are matched correctly and care instructions are followed, you can expect 25–50 industrial washes. But if the base knit shrinks even 3% after the film is applied, the film will buckle and fail within 10 cycles.
In the world of safety apparel, 3M Scotchlite™ is the gold standard. It is the benchmark against which all other reflective materials are measured. However, for many B2B brands, 3M’s pricing, MOQs, and distribution restrictions make it inaccessible or unprofitable.
This has led to a booming market for “3M equivalent” or “3M grade” reflective fabrics. But what does that actually mean? Technically, it means the material meets the same retro-reflection coefficients specified in standards like EN ISO 20471 or ANSI/ISEA 107.
When “equivalent” holds up:
When it doesn’t:
The decision framework is simple: if you are making high-risk safety gear for construction or traffic control, specify the genuine article or a rigorously tested alternative. If you are making running vests or fashion jackets, a qualified generic film on a quality knit substrate can deliver acceptable performance at 40–60% lower cost.
The demands on reflective knit fabric vary wildly depending on the end use. A fashion designer might want a subtle shimmer for a night-out jacket, while a construction worker needs maximum brightness to survive a night shift on the highway.
| Segment | Key Requirement | Recommended Type | Standard |
|---|---|---|---|
| Road Running | Stretch, Breathability, Visibility | Glass Bead on Jersey | EN 20471 Class 1 |
| Cycling | Aerodynamics, 360° Visibility | Prismatic on Mesh | EN 1150 |
| Industrial Workwear | Durability, Wash Cycles, Abrasion | Prismatic on Rib/Interlock | EN 20471 Class 3 |
| Children’s Outerwear | Safety, Soft Hand, Non-toxic | Glass Bead on Fleece | EN 14682 |
| Fashion / Streetwear | Aesthetics, Drape, Cost | Printed Reflective Ink | N/A |
Let’s look at a specific case study from the industrial sector. A European workwear manufacturer needed to upgrade their Class 3 hi-vis parka. They switched from sewn-on tape to laminated reflective knit panels for better comfort. The initial samples passed retro-reflection tests perfectly.
However, after simulated wear testing (Martindale abrasion), the prismatic film on the elbows and shoulders showed micro-cracking. The cause? The base knit they chose was too loose (a standard single jersey), allowing the film to flex beyond its limits at stress points.
The Fix: They switched to a firmer substrate—a 28-gauge 1×1 rib—and used a slightly thicker adhesive layer to act as a shock absorber. This reduced the initial brightness by 5% but increased the abrasion resistance by 400%. It was a necessary compromise for durability.
On the other end of the spectrum, “reflective fabric by the yard” is a huge search term for independent designers. While these buyers rarely need EN certification, they still face issues. I once saw a designer ruin a whole collection because she ironed directly over the reflective panels, melting the glass beads into a dull grey mess.
For those looking to understand the technical testing behind these applications, the knowledge base offers detailed guides on textile testing methods and compliance standards.
Sourcing technical textiles is risky. With reflective knit, the risks are amplified because you are bonding two different materials that have different physical properties. Here is a checklist to protect your supply chain.
The “split-supplier” risk is real. If the film peels off, the knit mill blames the laminator, and the laminator blames the adhesive supplier. To avoid this, look for manufacturers who control the process end-to-end.
| Risk | Impact | Mitigation |
|---|---|---|
| Film Delamination | Product Recall / Returns | Wash test samples 50x before bulk |
| Low Retro-reflection | Compliance Failure | Verify lab reports match your color/substrate |
| Adhesive Bleed-through | Aesthetic Defect | Check adhesive viscosity and cure temp |
| Color Mismatch | Rejection at QC | Approve lab dips under D65 light |
Regarding MOQs: stock reflective fabrics usually start at 500 m (547 yd). However, if you need a specific base fabric—say, a particular weight or color—with custom lamination, expect to commit to 2,000 m (2,187 yd) or more. Some suppliers offer sample Garment Yardage Calculator programs (50–100 m / 55–109 yd) for development, which is worth asking about.
If you are ready to start the conversation, you can submit your specifications and CAD files through the contact form, and a technical engineer will assess feasibility and provide a quotation.
You can source the best reflective knit fabric performance material in the world, but if the end consumer washes it wrong, it will fail. As a brand, you are responsible for the care label.
Reflective films are sensitive to heat, chemicals, and mechanical agitation. The care instructions must be specific to the film technology used.
| Parameter | Glass Bead Film | Prismatic Film |
|---|---|---|
| Max Wash Temp | 60°C (140°F) | 40°C (104°F) to 60°C (140°F) |
| Tumble Dry | Low Heat / No Heat | No / Line Dry |
| Bleach | No Chlorine Bleach | No Chlorine Bleach |
| Dry Cleaning | Solvent Only | Not Recommended |
| Ironing | No Steam / Low Temp | Do Not Iron over film |
A critical legal point: under EN ISO 20471, the garment must remain compliant for the number of washes stated on the care label. If you label it “Wash 50 times,” but the reflective film fails at 30, you are liable. It is better to be conservative. If your testing shows 40 cycles, label it for 25.
I recommend including a small icon or warning on the care label: “Do not iron directly over reflective panels.” It seems obvious, but you would be surprised how many returns happen because someone scorched their vest with a hot iron.
A performance knit fabric is any engineered textile designed to deliver functional properties beyond basic coverage. In the context of reflective materials, it refers to a knit construction (like rib, interlock, or mesh) that provides the necessary stretch, recovery, and surface smoothness to support a reflective film layer without compromising the wearer’s comfort or range of motion.
Technically, the correct term is “retro-reflective fabric.” This distinguishes it from standard reflective materials (like a mirror) which scatter light. In spec sheets, you might also see “high visibility reflective fabric” (implying compliance with safety standards) or “silver reflective fabric” (describing the color of standard glass bead films).
With proper construction and care, laminated reflective knit fabric can maintain its retro-reflective properties for 25 to 50 industrial wash cycles. Budget or poorly laminated films may fail in under 10 cycles. Longevity depends heavily on the base knit’s stability, the adhesive quality, and strict adherence to care instructions.
Generally, no. The reflective film is applied to a pre-dyed base fabric. Applying heat or pressure for printing post-lamination will damage the optical structures. However, some manufacturers offer colored reflective films (red, blue, fluorescent yellow) that are incorporated during the lamination process, allowing for design flexibility without post-printing.
Specifying reflective knit fabric is a balancing act. You are constantly trading off brightness for flexibility, durability for cost, and compliance for aesthetics. The perfect fabric doesn’t exist, but the right fabric for your specific application does.
Don’t rely on swatches alone. Demand data. Wash the samples. Stretch them. Scrutinize the test reports. The glow-in-the-dark effect is cool, but the engineering underneath is what keeps your customers safe and your brand reputation intact.