Address
Nanlang Industrial Zone, Xingtan Town, Shunde District, Foshan, Guangdong, China
Work Hours
Mon–Fri, 9:00 AM – 6:00 PM (CST/UTC+8). We aim to respond to all inquiries within 48 hours.

Address
Nanlang Industrial Zone, Xingtan Town, Shunde District, Foshan, Guangdong, China
Work Hours
Mon–Fri, 9:00 AM – 6:00 PM (CST/UTC+8). We aim to respond to all inquiries within 48 hours.
Best Fabrics for Yoga Clothing: A Performance & Comfort Breakdown. This guide covers key properties, real-world applications, and a practical sourcing checklist for B2B buyers.
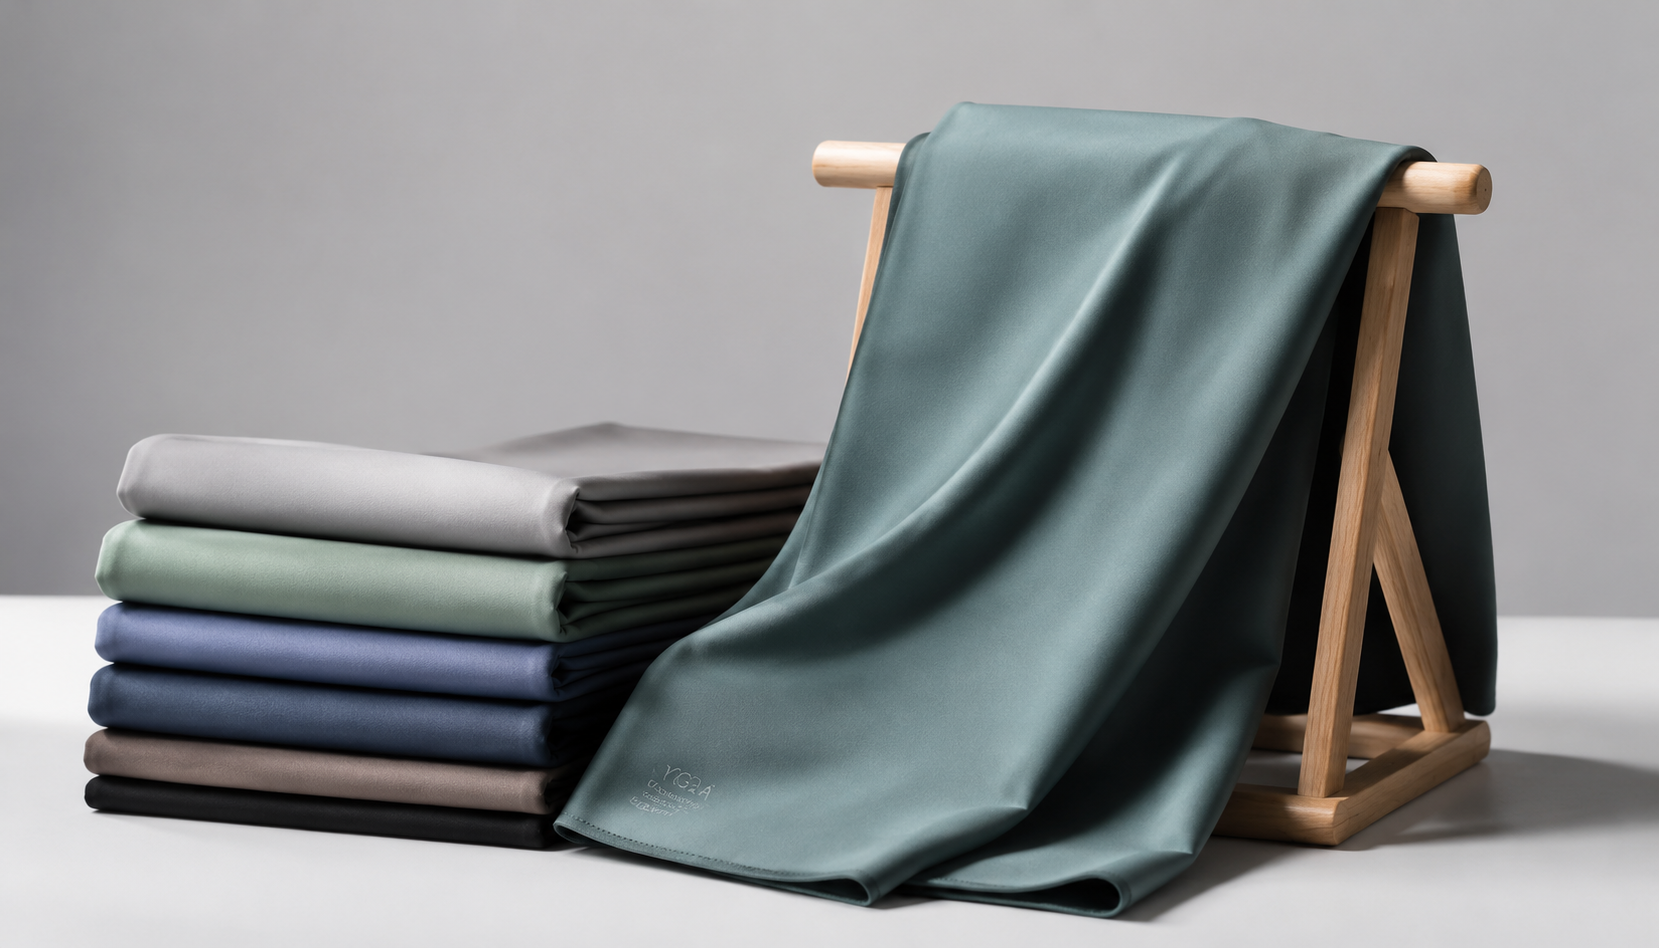
A brand’s sourcing manager once told me she picked a “four-way stretch Nylon-Spandex” for their debut yoga leggings line based on swatch feel alone. Three weeks after the first production run hit shelves, the complaints started rolling in — the fabric bled color in hot yoga sessions, balled up at the inner thighs after five washes, and turned slightly translucent in downward dog. The entire 12,000-unit batch had to be marked down by 60% to clear inventory. That single mistake cost the brand nearly $180,000 and six months of lost momentum.
The takeaway isn’t that the fabric was inherently bad. It’s that nobody stress-tested it against the specific biomechanical and environmental demands of yoga practice. Choosing the best fabrics for yoga clothing isn’t about picking the “softest” or “most elastic” option off a sample card — it’s about matching fiber chemistry, knit construction, finishing treatments, and performance testing data to a clearly defined product tier and use case.
This guide breaks that process down, step by step.
Here’s the problem with most fabric selection checklists: they treat yoga like any other sport. It isn’t.
Running and HIIT are dominated by continuous, high-impact movement — your fabric needs to manage sweat volume and resist abrasion at maximum intensity. Yoga, on the other hand, cycles between dynamic flow sequences (think vinyasa transitions at 90-second intervals) and static holds (warrior II at 45 seconds, pigeon pose at two minutes). The fabric must perform across both modes simultaneously.
That means you’re engineering for four qualities at once, not one:
This dual-mode requirement is what makes yoga pant fabric selection genuinely difficult. Get the balance wrong, and you end up with leggings that feel amazing during sun salutations but leave the wearer cold and clammy during the closing sequence.
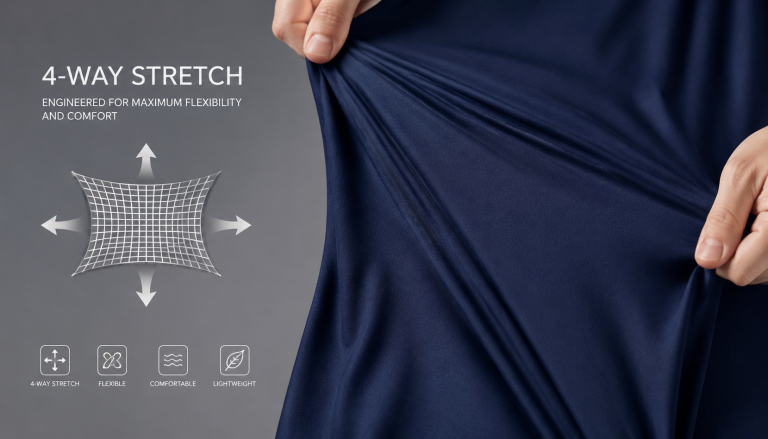
A surprisingly common procurement mistake: assuming that “stretchy” equals “four-way stretch.” It doesn’t.
Weft-knit constructions — single jersey, interlock, and their derivatives — naturally provide mechanical stretch in both directions because of their looped interlocking structure. The stretch is inherent to the knit geometry, not dependent on fiber content alone.
Woven fabrics, by contrast, achieve stretch primarily through the incorporation of elastane (spandex) fibers. A woven stretch fabric might deliver 15–25% elongation in the weft direction but only 3–8% in the warp. That’s functionally two-way stretch — fine for a structured blazer, inadequate for yoga.
The real danger lies in testing: many buyers pull the fabric by hand and declare it “stretchy enough.” What they should be measuring is 30-cycle recovery rate — stretch the fabric to 20% elongation, release, repeat 30 times, and measure the residual deformation. Anything less than 90% recovery after 30 cycles will show visible bagging within the first month of regular wear. For the best fabrics for yoga clothing, you need ≥92% recovery. Period.
| Performance Dimension | Yoga Requirement | Running Requirement | HIIT Requirement |
|---|---|---|---|
| Stretch direction | Four-way (all poses) | Primarily longitudinal | Four-way (multi-plane) |
| Recovery rate (20% elongation) | ≥92% | ≥85% | ≥90% |
| OMMC (moisture management) | ≥2.5 (moderate flow) to ≥3.5 (hot yoga) | ≥3.5 | ≥4.0 |
| Thermal comfort at rest (Clo value) | 0.4–0.6 | Not critical | Not critical |
Now that we’ve established the performance framework, let’s look at what each fiber actually brings to the table — and where it falls short. I’ll evaluate each on the same five dimensions: elasticity, moisture management, hand feel, durability, and cost range.
There’s a reason the vast majority of premium yoga leggings use Nylon 66 blended with 15–22% spandex. Nylon 66 offers abrasion resistance that’s roughly 2.5× better than standard polyester at equivalent Yarn Count Converter — critical for the inner thigh contact zone that takes constant friction during every fold and transition.
Typical blend ratios — 80/20 or 78/22 Nylon/Spandex — deliver four-way stretch with superior recovery. The spandex provides the snap-back; the nylon provides the structural backbone and abrasion defense. Nylon also dyes deeply and cleanly, which matters when your brand palette includes jewel tones and saturated colors.
The downside? Nylon hydrolysis under extreme conditions — prolonged UV exposure combined with high humidity can degrade the polymer chain over 12–18 months. For yoga practitioners who air-dry their leggings in direct sunlight, this is a real factor.
Polyester’s hydrophobic nature — it absorbs less than 0.4% moisture by weight, compared to nylon’s ~4% — means sweat doesn’t saturate the fiber itself. Instead, moisture is transported along the fiber surface through capillary action in the knit structure, then evaporates rapidly. In hot yoga scenarios, polyester-spandex consistently outperforms nylon-spandex in drying time by 20–30%.
The trade-off is tactile. Raw polyester has a slightly plasticky hand feel that most consumers instinctively reject in a fitting room. The solution lies in two engineering approaches:
For Spandex Yoga pants targeting the mass market ($30–$55 retail), polyester-spandex blends at 85/15 or 88/12 ratios offer the best cost-to-performance ratio. Just budget for the finishing investment.
Modal, a regenerated cellulose fiber derived from beechwood pulp, offers something no synthetic can match: an inherently silk-like hand feel without any finishing treatment. Its moisture regain of ~12% (versus nylon’s 4% and polyester’s 0.4%) gives it a naturally comfortable, breathable quality that resonates with practitioners who prioritize skin sensation over peak athletic performance.
But here’s the honest assessment: Modal’s wet tensile strength drops to roughly 40–50% of its dry value. That’s a serious limitation for yoga leggings that need to survive repeated wash cycles without losing shape. Modal fabric performs best in upper-body garments — tank tops, bralettes, lightweight wraps — where the mechanical stress is lower and the skin-contact luxury is the primary selling point.
For leggings? Pure Modal is rarely the answer. A Modal-Nylon-Spandex tri-blend (40/40/20, for example) can deliver the soft hand feel while borrowing structural integrity from the synthetic components. But cost creeps up, and color consistency across fiber types during dyeing becomes a production headache.
Let’s address this directly, because the yoga market is saturated with bamboo marketing claims that don’t survive scrutiny.
Chemical bamboo viscose — which accounts for 99%+ of “bamboo fabric” on the market — is produced through the same viscose process used for any wood-pulp-based rayon. The bamboo plant’s natural antimicrobial properties (attributed to a compound called “bamboo kun”) are destroyed during the sodium hydroxide and carbon disulfide processing. What you’re left with is, functionally, rayon made from bamboo pulp rather than pine or eucalyptus pulp. The performance difference is negligible.
Mechanical bamboo fiber — where the plant is physically crushed and enzymatically processed to extract intact fibers — does retain some natural properties. But global production capacity is tiny (estimated at under 5,000 metric tons per year, compared to 5+ million tons for standard viscose), and pricing is 3–5× higher than conventional viscose.
If your brand story requires a “bamboo” component, buy bamboo viscose with clear eyes about what it actually is. Don’t let suppliers charge a premium for performance claims that vanish under the AATCC 195 moisture management test.
Cotton in yoga apparel sounds counterintuitive — it absorbs moisture like a sponge, takes forever to dry, and loses shape rapidly under repeated stretch. All true. But in the restorative yoga market (think Yin, gentle flow, meditation-focused classes), cotton’s profile actually makes sense: warm, soft, breathable during low-intensity holds, and comfortable enough to wear all day as loungewear.
Organic cotton certified to the GOTS (Global Organic Textile Standard) opens access to the premium conscious-consumer segment willing to pay $60–$90+ for yoga pants. The caveat: organic cotton supply chains have real constraints. Minimum order quantities from certified mills typically start at 3,000–5,000 meters per color, and lead times stretch to 45–60 days for dyeing and finishing.
My honest take: cotton-spandex yoga leggings occupy a legitimate niche, but trying to position them as high-performance activewear is a recipe for returns and complaints.
The recycled fiber landscape has matured dramatically over the past five years. Recycled polyester (rPET) from post-consumer bottles now achieves tensile strength and elongation figures within 2–5% of virgin polyester. Recycled nylon (rNylon), primarily sourced from abandoned fishing nets and industrial waste through programs like ECONYL®, performs virtually identically to virgin Nylon 6 in most applications.
The procurement reality: GRS (Global Recycled Standard) 4.0 certification is now a baseline requirement for most European and North American yoga brands. It’s not optional. Ensure your supply chain can provide batch-level traceability documentation — GRS scope certificates, transaction certificates, and chain-of-custody records.
The tricky part is color consistency. Recycled fiber feedstock varies from batch to batch in terms of residual color and chemical composition. Expect a slightly wider dye lot variation (Delta E of 1.5–2.5 versus 0.5–1.0 for virgin fibers) unless the supplier applies additional pre-treatment steps.
| Fiber / Blend | Recovery Rate | Moisture Mgmt | Hand Feel | Relative Cost |
|---|---|---|---|---|
| Nylon 66 + Spandex (80/20) | 92–96% | Moderate | Smooth, cool | $$$ |
| Polyester + Spandex (85/15) | 88–94% | Excellent | Moderate (finishing-dependent) | $$ |
| Modal (100%) | 70–80% | Good | Silk-like, luxurious | $$$ |
| Bamboo Viscose + Spandex | 75–85% | Good | Soft, drapes well | $$–$$$ |
| Cotton + Spandex (92/8) | 60–75% | Poor | Warm, familiar | $ |
| rPET + Spandex (85/15) | 88–93% | Excellent | Finishing-dependent | $$–$$$ |
This is the part most procurement teams skip, and it’s arguably where the biggest quality gaps hide. Two fabrics made from identical Nylon 66 / 20% Spandex yarns can feel — and perform — completely differently depending on how they’re knitted. The same fiber is not the same fabric.
The two broad families relevant to yoga apparel are weft knits (where yarns run horizontally) and warp knits (where yarns run vertically along the fabric length). Within each family, specific constructions create distinct physical properties.
These three weft-knit constructions dominate the yoga leggings market, each occupying a distinct performance and price tier.
Single jersey is the lightest and most economical option — a simple face/back loop structure that produces a fabric with excellent drape and soft hand feel. Typical weight: 150–180 gsm (4.4–5.3 oz/yd²). The problem: single jersey is inherently unbalanced in its loop structure, which means it curls at the edges when cut. For yoga leggings, this curling manifests as leg hems that roll up during practice — a constant nuisance that consumers notice immediately. It also offers the least dimensional stability of the three.
Interlock is a double-knit construction where two single jersey faces are interlocked — imagine two layers of jerseys stitched through one another. The result is a thicker, more stable fabric that resists curling, provides better opacity (critical for squat-proof performance), and recovers more uniformly. Typical weight: 200–260 gsm (5.9–7.7 oz/yd²). Interlock is where the majority of mid-premium yoga leggings live.
Ponte di Roma (commonly just “ponte”) is a double-knit construction using two sets of needles that create a firm, structured fabric with a smooth face and subtle texture on the back. Typical weight: 260–320 gsm (7.7–9.4 oz/yd²). Ponte’s rigidity makes it less ideal for high-flexibility yoga poses but excellent for yoga pants designed to double as streetwear — ponte holds a clean silhouette without compression.
Here’s a simplified decision path that captures the core logic:
Warp knits — specifically tricot and raschel constructions — represent a fundamentally different approach to fabric engineering. Instead of relying on yarn loops that interlock in rows (weft knit), warp knit structures use parallel yarns that interlock in columns. The result: significantly less stretch (typically 15–30% versus 50–80% for weft knits) but dramatically higher dimensional stability and resistance to runs and snags.
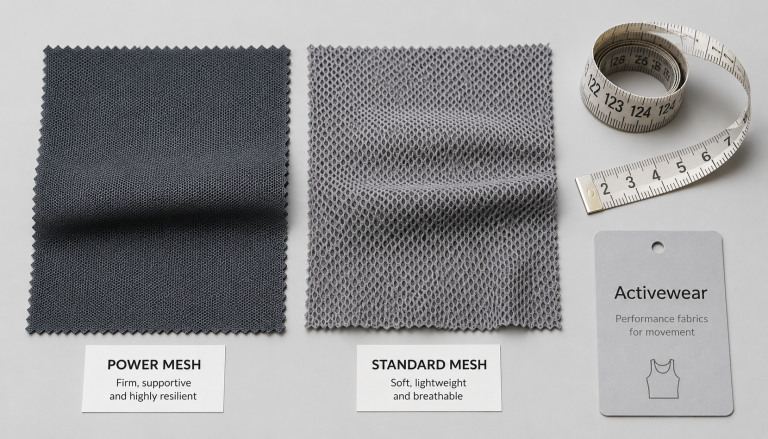
In the yoga apparel context, warp knit mesh performance fabrics are finding traction in sports bras, crop tops, and ventilation panels where controlled support matters more than extreme stretch. A cooling mesh tricot with strategic perforation zones can manage airflow during hot yoga without the fabric collapsing against the skin during inversions — something a soft weft-knit mesh cannot guarantee.
For Yoga Pant fabric specifically — meaning the legging itself — weft knit remains the dominant construction. But smart designers are incorporating warp knit panels in targeted zones: a tricot-knit waistband for structural hold, raschel mesh inserts at the calves for ventilation. It’s a hybrid approach that borrows the best qualities of both construction families.
If you take one section from this article back to your product development team, make it this one. Performance testing separates fabrics that merely look good on a swatch card from fabrics that survive real-world yoga practice.
Below are the non-negotiable tests for yoga apparel fabrics. Not “nice to have” — non-negotiable. If your supplier can’t provide these results, you’re operating blind.
The ASTM D4964 standard governs stretch testing for textile fabrics. The critical metric: at 20% elongation, the recovery rate must be ≥90% after a single cycle. Multi-cycle testing (30 cycles at 20% elongation) should show ≥90% recovery as well — this simulates the cumulative stretching a yoga pant experiences across 30 wear-wash cycles.
Any fabric that drops below 88% recovery at the 30-cycle mark will show visible knee bagging and seat sagging within six to eight weeks of regular use. For best fabrics for yoga clothing, push for ≥92% at 30 cycles. That’s the threshold where the consumer perceives the garment as “holding its shape.”
AATCC 195 measures liquid moisture management capability (OMMC) using a sweating guarded hot plate or, more commonly in production environments, a moisture management tester (MMT). The test measures how quickly moisture spreads across the fabric surface (wetting time), how fast it moves through the fabric to the outer face (absorption rate), and the speed at which the outer face dries (drying rate).
For standard vinyasa-class yoga (moderate sweat output), an OMMC of ≥2.5 is acceptable. Hot yoga — where sweat rates can reach 1.0–1.5 liters per hour — demands ≥3.5. Fabrics scoring below 2.0 will feel wet and clingy within 15 minutes of practice.
The factory’s moisture-wicking fabric line is specifically engineered to achieve OMMC values in the 3.0–4.5 range through controlled fiber denier variation and specialized knit geometries that create capillary channels.
Pilling on yoga leggings is not a cosmetic issue alone — it signals fiber fragmentation that weakens the fabric surface over time. The ASTM D4970 Martindale abrasion test subjects the fabric to circular rubbing under standardized pressure and counts the cycles until pilling visually appears.
For yoga leggings, the minimum acceptable score is 4 on a 5-point pictorial scale after 5,000 Martindale cycles. Premium brands typically specify ≥20,000 cycles with no visible pilling below grade 4. The inner thigh zone — where leg-to-leg friction occurs hundreds of times during a single class — is the failure hotspot. Nylon-spandex consistently outperforms polyester-spandex on this metric due to nylon’s superior abrasion resistance at the molecular level.
| Test Parameter | Standard | Minimum Threshold | Premium Target |
|---|---|---|---|
| Stretch recovery (30 cycles, 20% elongation) | ASTM D4964 | ≥88% | ≥92% |
| OMMC (hot yoga) | AATCC 195 | ≥3.0 | ≥3.5 |
| Pilling resistance (Martindale cycles) | ASTM D4970 | 5,000 cycles ≥ Grade 4 | 20,000 cycles ≥ Grade 4 |
| Color fastness to washing (5 cycles) | ISO 105-C06 | Grade 3–4 | Grade 4–5 |
| Dimensional stability (5 washes) | AATCC 135 | ≤±3% shrinkage | ≤±2% shrinkage |
Technical specifications in isolation are useless without a decision framework that ties them to your product strategy. This is where most sourcing guides break down — they dump a pile of fiber chemistry facts without connecting them to the business realities of price points, lead times, and brand positioning.
The framework below maps three product tiers to their optimal fiber selection, blend ratio, target weight, and cost band. It’s not a rigid prescription — local market conditions, brand identity, and competitive positioning all factor in — but it provides a starting architecture that prevents the most common mismatches.
| Product Tier | Primary Fiber Selection | Typical Blend Ratio | Target Weight | Cost (FOB per meter) |
|---|---|---|---|---|
| Premium ($70–$130 retail) | Nylon 66 + Lycra® / LYCRA® SPORT | 78/22 or 75/25 | 220–260 gsm (6.5–7.7 oz/yd²) | $5.50–$12.00 |
| Mass Market ($30–$65 retail) | Polyester + Spandex | 85/15 or 88/12 | 180–220 gsm (5.3–6.5 oz/yd²) | $3.00–$6.00 |
| Budget ($15–$30 retail) | Standard Nylon + Spandex or Cotton-Spandex | 82/18 or 92/8 | 160–200 gsm (4.7–5.9 oz/yd²) | $1.80–$4.00 |
When evaluating suppliers, ask to see their complete performance functional knits catalog — from wicking fabrics to antimicrobial options to temperature-regulating constructions. A supplier’s breadth in this category tells you a lot about their R&D investment and whether they can support you as your product line evolves.
Numbers on a spreadsheet mean nothing if production can’t deliver on time and on budget. Here’s what the actual procurement timeline looks like for functional knit fabrics used in yoga apparel.
Sample MOQ for most knitted performance fabrics is 1–3 meters (1.1–3.3 yd) per colorway, delivered in 3–5 business days for stock items. Custom lab-dip development adds 5–7 working days.
Bulk MOQ for performance functional knits generally starts at 500 meters (547 yards) per colorway. Some suppliers — particularly those with a 2,000-square-meter finished goods warehouse holding stock inventory — can accommodate 300-meter (328-yard) orders for pre-developed SKUs. Custom developments with specialized finishing (e.g., cooling finish, antimicrobial treatment) typically require 1,000+ meters (1,094+ yards) minimum.
Lead times break down as follows:
If you have a specific yoga fabric project in development and want to discuss technical feasibility, blend optimization, or sampling timelines, the factory’s engineering team can be reached through their contact page, where you can upload spec sheets and receive a feasibility assessment within 24 business hours.
European and North American yoga brands will request certifications before they place their first order. Here’s the hierarchy, from “you cannot ship without this” to “this differentiates you from competitors”:
The factory behind this guide has operated since 2005 with the full certification matrix above — OEKO-TEX Standard 100, GRS 4.0, ISO 9001, and EU REACH compliance — supporting brands across North America, Europe, and Asia-Pacific. The about page provides a comprehensive view of the manufacturing infrastructure and quality systems that underpin these credentials, including the 2,000-square-meter stock warehouse and integrated weaving-dyeing-finishing production line.
This is the kind of story that doesn’t make it into supplier presentations but reveals more about fabric selection than any spec sheet ever will.
A mid-size DTC yoga brand based in Southeast Asia launched a “Hot Yoga Pro” collection in Q3 2023. The brief was clear: high stretch, fast drying, comfortable enough for a 90-minute Bikram session at 40°C (104°F). The product development team evaluated two candidate fabrics — a Nylon 66/Spandex 80/20 blend at 220 Fabric GSM Calculator (6.5 oz/yd²) and a Polyester/Spandex 88/12 blend at 160 gsm (4.7 oz/yd²).
The nylon option tested well on every parameter: OMMC of 3.2, stretch recovery of 94% after 30 cycles, pilling score of 4.5 after 10,000 Martindale cycles. But it cost $7.20 per meter. The polyester option scored similarly on moisture management (OMMC 3.7, actually better) and cost $3.80 per meter — nearly half.
The CFO overruled the product team. Price won.
First production run: 5,000 units cut and sewn from the 160 gsm polyester-spandex. Within two weeks of launch, the complaints hit:
The brand dropped their retail price by 40% to clear the inventory. Total loss on the first batch: approximately $120,000 when accounting for the markdown, returns processing, and damaged customer trust.
For round two, they went back to the Nylon 66/Spandex 78/22 blend — but with three specific modifications informed by the failure:
Per-meter cost rose to $8.60 — about 18% above the original nylon quote, due to the enhanced finishing. Unit cost went up accordingly. But the results spoke decisively: return rate dropped from 22% to under 3%, the average review score climbed from 3.1 to 4.6 stars, and the brand was able to raise the retail price by 15% on the strength of the improved product reputation.
The core lesson: saving $3.40 per meter on fabric cost generated a $120,000 loss. Spending $1.40 more per meter on the right fabric generated a product that commanded a 15% retail premium. The math isn’t complicated — but it requires treating fabric selection as an engineering decision, not a procurement exercise.
The majority of yoga apparel revenue still flows through women’s product lines, and the fabric performance requirements for women’s garments are measurably more demanding than men’s. Here’s why.
Women’s yoga leggings must pass the “squat-proof” test — the fabric cannot become translucent when stretched to 90%+ elongation over the glute and quad areas. This alone eliminates many sub-200 gsm (5.9 oz/yd²) fabrics that would otherwise perform adequately. The typical weight band for premium women’s yoga leggings sits at 220–260 gsm (6.5–7.7 oz/yd²), constructed in interlock or double-jersey to maximize opacity.
High-waist construction — now the dominant design in women’s yoga pant fabric — demands a waistband fabric with exceptionally high recovery (>95% at 30% elongation) to maintain compression and prevent rollover during dynamic movements. This typically means the waistband zone uses a higher spandex content (22–25%) than the leg body panels (15–20%). Yoga Pant fabric for women also needs to address the hip and glute contour — a slight compression grade that flatters without restricting hip-openers and deep lunges.
Men’s yoga clothing leans toward looser silhouettes — jogger-style pants, relaxed-fit shorts, and drape-heavy tops. The fabric priorities shift accordingly:
The best fabrics for yoga clothing targeted at men tend to be polyester-spandex or lighter-weight nylon-spandex constructions with open-mesh ventilation zones — a fundamentally different engineering approach than the high-opacity, high-compression fabrics that dominate women’s yoga leggings.
There is no single “best” material — the answer depends entirely on your product’s position in the market and the yoga practice it’s designed for. For premium lines targeting serious practitioners, Nylon 66 blended with 20–22% spandex (at 220–260 gsm / 6.5–7.7 oz/yd²) remains the gold standard for yoga leggings, delivering the best balance of recovery, abrasion resistance, and hand feel. For mass-market yoga pants, polyester-spandex at 85/15 with peach finishing offers the best value proposition. The decision should start with your product tier, then work backward to fiber and construction selection. This article’s supply decision matrix provides the detailed framework.
Activewear is a broad category — yoga, running, cycling, gym training, and outdoor sports all have radically different fabric requirements. The best fabrics for activewear in a general sense share common traits: four-way stretch, moisture management, and durability through wash cycles. But the specific optimization targets differ. Running apparel prioritizes moisture-wicking speed (OMMC ≥3.5) and lightweight construction (100–160 gsm / 2.9–4.7 oz/yd²). Gym training apparel prioritizes abrasion resistance and squat-proof opacity. Yoga apparel uniquely requires thermal comfort during static holds — a parameter that’s irrelevant in most other activewear categories. Always select fabric based on the specific sport and use case, never on “activewear” as a generic category.
“Healthiest” requires two definitions. First, skin safety — any fabric certified to OEKO-TEX Standard 100, Class II has been tested for harmful chemical residues including formaldehyde, heavy metals, and restricted azo dyes. This certification is the health baseline for all skin-contact textiles. Second, environmental health — GRS-certified recycled fibers reduce dependence on virgin petrochemical feedstocks, while organic cotton (GOTS certified) eliminates pesticide residues in the growing and processing stages. Modal fabric from sustainably managed beechwood forests offers excellent biodegradability. The honest reality is that synthetic performance yarns (nylon, polyester) remain superior for functional yoga leggings, but look for suppliers who combine performance synthetics with responsible chemistry and certified recycled content.
From a functional textile perspective, yoga clothing must satisfy three simultaneous requirements: unrestricted movement (four-way stretch with ≥90% recovery), sweat management (moisture transport away from skin without leaving the wearer soaked), and thermal balance (warm enough during restorative holds, cool enough during dynamic flow). Converting those functional requirements into actual fabric specifications, you’re looking at an interlock-knit Nylon 66/Spandex blend at 200–240 gsm (5.9–7.1 oz/yd²) with OMMC ≥2.5 for standard practice or OMMC ≥3.5 for hot yoga. The fabric should feel like a second skin — noticeable only when it fails. Anything the practitioner has to think about during class — riding waistbands, sticky thigh panels, visible sweat patches — represents a fabric engineering shortfall.
For deeper technical resources on fiber properties, knit construction methodology, and finishing processes, the factory’s knowledge base offers an ongoing library of fabric technology articles written specifically for sourcing professionals and product developers.
Fabric selection for yoga apparel is an engineering problem disguised as an aesthetic one. Every decision — fiber chemistry, blend ratio, knit structure, weight, finishing treatment — cascades into the product’s real-world performance in ways that only become visible after 20 wears, 10 washes, and three months of use. By which point, of course, it’s far too late to change course without significant cost.
The brands that consistently win in this category don’t do it by choosing the softest swatch or the cheapest quotation. They do it by building a testing protocol that mimics actual yoga practice — static holds in heated rooms, deep-stretch recovery under sustained elongation, pilling resistance at friction hotspots — and refusing to approve any fabric that hasn’t passed every test in the protocol.
Start with the four-dimensional framework articulated at the top of this article: stretch, recovery, moisture management, thermal comfort during stillness. Test against real-world thresholds, not supplier promises. Validate with wear trials on actual bodies, not just lab instruments. The best fabrics for yoga clothing are the ones that disappear into the practice — and that kind of invisibility takes deliberate, rigorous engineering to achieve.